The first export shipment can fail commercially even when the power tools themselves function correctly. A crushed retail carton, cracked case, loose battery or missing accessory can make an item unsaleable at the destination. A packaging test gives buyers a way to challenge a proposed carton before thousands of units are packed. It should use the real product, inserts and transport configuration, and it should answer a defined damage question—not merely generate a photograph of a box after one arbitrary drop.
This article gives importers a practical planning framework. It is not a substitute for a packaging engineer, carrier rules or the full text of a test protocol. No single test guarantees damage-free delivery. The aim is to select a relevant method, record the product's condition before and after, correct weaknesses, and keep the tested package configuration under control through shipment.
Define what must arrive saleable
List the contents of the retail pack and how each could be damaged. A corded drill may need protection for its chuck, side handle and cable. A grinder may have a guard and wheel accessory that can shift in the box. A chainsaw has a bar, chain and protective cover. A planer has a cutterhead, blade and sole that should not carry transport impact directly. A cordless kit adds battery and charger positioning. The acceptance criterion should cover the tool, accessories, case, retail box and readable labels.
Distinguish consumer-facing presentation from outer export packaging. A master carton may protect several retail units, but cartons can be split during distribution and individual units may travel to an e-commerce customer later. Decide which packaged level is being tested and why. A test on a master carton does not automatically prove the retail pack can survive single-parcel shipping.
Specify the route: sea freight with pallet handling, air freight, parcel delivery or a combination. The likely handling and climate exposure differ. A logistics partner and packaging specialist should select the applicable test method. The International Safe Transit Association's ISTA 1A overview describes a sequence involving conditioning, vibration and shock for certain packaged products up to its stated weight limit. That overview illustrates the need for a sequence, not an instruction to apply ISTA 1A to every ToolViron product without checking fit.
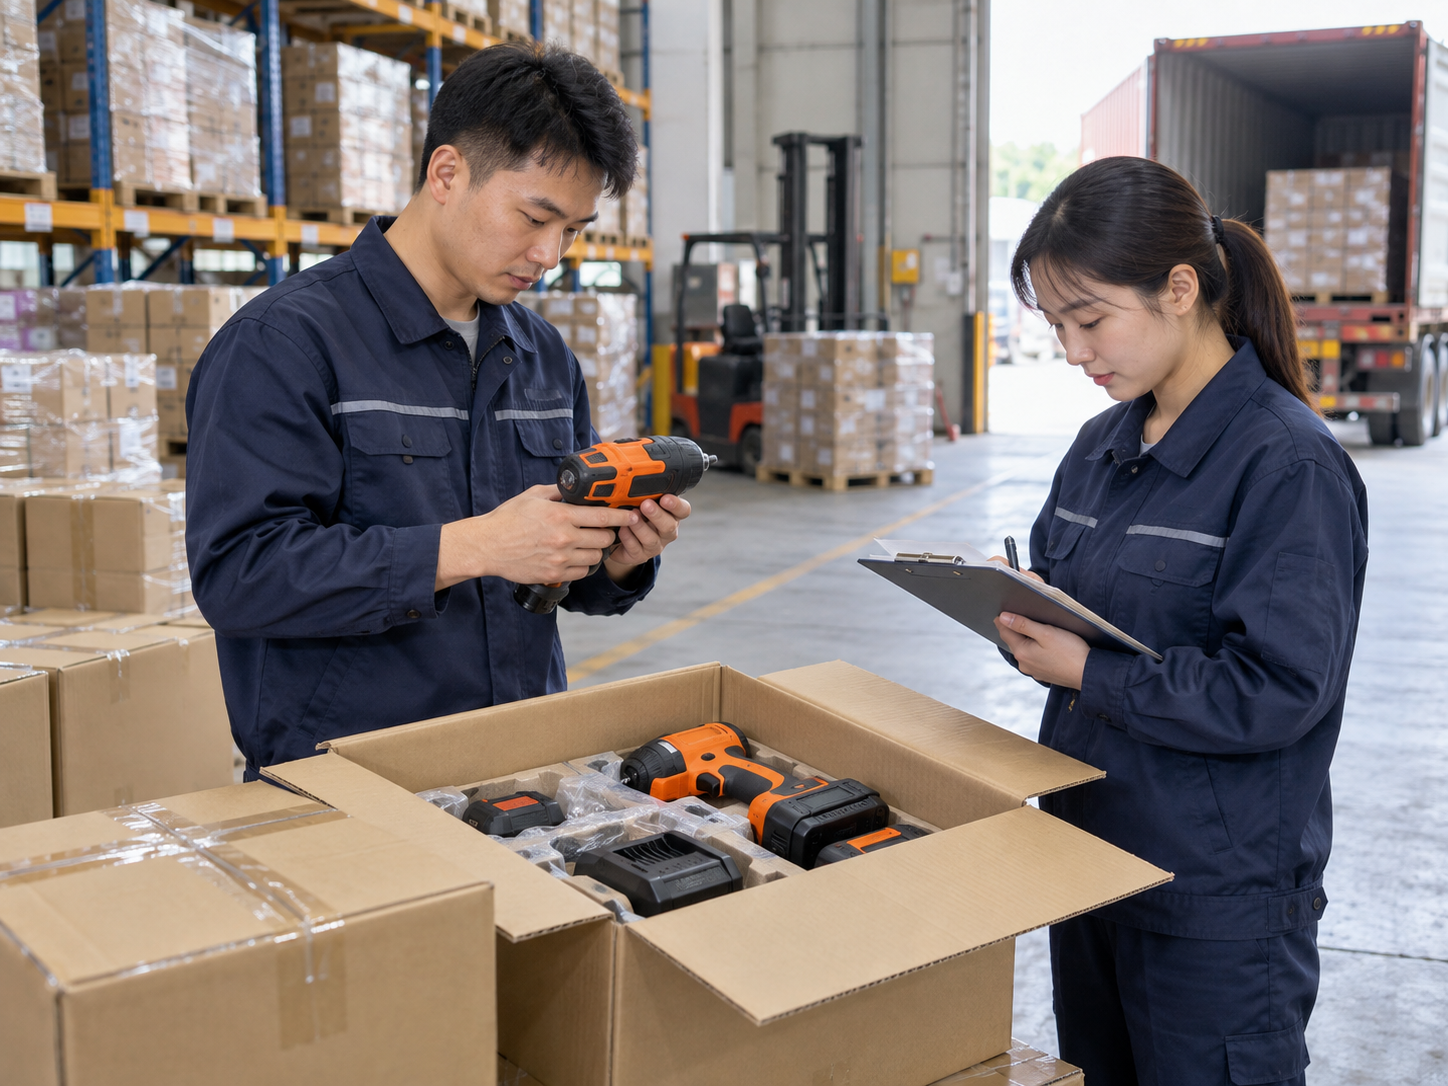
Caption: A packaging review should inspect both the product and the customer-facing carton after the defined handling sequence.
Test the production-intent pack, not a design mock-up
Use the exact tool and all promised accessories, insert materials, bags, case, manual, retail carton, tape and master carton intended for production. Prototype foam cut by hand or a stronger sample carton may not represent the actual packing line. Record component dimensions, material specifications and supplier revisions so the tested assembly can be repeated. If a cardboard grade or insert shape changes after approval, the result may no longer apply.
Assemble the package the way factory staff will. Photograph the open pack, label positions and each product contact point. Check whether a heavy battery can move and strike the tool, whether a chainsaw bar can puncture the carton, or whether a sharp accessory can damage the manual. A package that passes an external drop but allows internal parts to rub and mark a housing may still fail the buyer's retail standard.
Record gross weight and dimensions at the tested level. A different carton count or pallet pattern changes loads and handling. If a kit variant adds a second battery, retest or at least perform a documented engineering assessment. Do not reuse the first variant's test report as proof for every heavier SKU in the range.
Choose a method and acceptance criteria before the drop
The test plan should name the standard or agreed method, packaged level, sample count, conditioning, sequence, orientation, impact energy or drop heights where applicable, and post-test inspection. These details should come from the chosen protocol and qualified packaging team, not a blog's universal number. Decide before testing whether cosmetic carton dents are acceptable, whether torn sealing tape is a failure, and what product damage is always unacceptable.
The post-test check should include function and product information, not only visual appearance. A drill chuck, grinder guard, chainsaw bar or planer depth control could be affected without an obvious carton puncture. A qualified reviewer should perform appropriate non-destructive checks and compare with the pre-test condition. Battery packs and chargers need particular care; do not perform unsafe ad hoc tests after a suspected impact.
If a package fails, preserve photographs and the damaged specimen. Change the insert, carton or packing sequence with a specific hypothesis, then repeat the appropriate test. Do not simply add layers of material until the box looks thick: extra weight, cost and size can harm freight economics without protecting the vulnerable point. The goal is controlled protection at an acceptable landed cost.
Mid-article sourcing CTA: Preparing a private-label export pack? Send the exact kit contents, retail channel and shipping route to discuss a production-intent packaging review.
Include vibration and stacking considerations
A single drop is only one part of transit. Vibration can move loose accessories, abrade a painted surface or loosen a bag. Stacking can deform cartons or cases. Humidity can weaken paper-based packaging. Select tests that reflect the route and distribution channel rather than calling one dramatic drop a complete validation. ISTA's overview is useful because it presents a sequence of stresses, but the relevant procedure should be chosen with the shipment's real mass and route in mind.
Check the customer-facing pack after the sequence. An outer master carton may be damaged while the retail unit remains saleable; that may be acceptable under an agreed criterion. The opposite is worse: a clean outer box can conceal a tool that shifted inside its case. Open packages and record the positions of all components. This helps determine whether the failure is an insert design, packing execution or carton-strength problem.
Packaging should also support shipment inspection. If the box cannot be opened and re-sealed without obvious damage, the inspection plan needs a method for sampled units. A design that prevents inspection is not necessarily safer; it can make quality verification and rework harder. The export-packaging guide covers the broader balance between presentation and transport, while this article focuses on test evidence.
Control artwork and safety information after redesign
A new insert or carton size can move labels, warnings or battery markings. After any packaging change, review all printed information and barcodes at full size. A smaller face may make a required warning unreadable or force a QR code into a fold. Product imagery should still show the actual contents. The manual-and-label localization guide describes this cross-check.
If lithium batteries are included, coordinate the final packing configuration with the carrier and relevant transport specialists. A package test does not establish that a shipment satisfies dangerous-goods requirements. The lithium-battery shipping guide addresses the separate information and carrier-approval workstream.
Keep a version-controlled packaging specification: drawing, material grade, insert layout, sealing method, carton marks, tested report and effective production lot. The factory should know which revision is approved. A supplier's cost-saving substitution of a thinner insert can invalidate the test result just as surely as a different tool component can invalidate a functional sample.
Verify packing during production and shipment inspection
During factory packing, check that the product sits in the approved orientation, accessories occupy their assigned positions and the correct insert and carton are used. A packaging design can be sound but fail because staff assemble it differently at speed. Create visual work instructions and spot checks appropriate to the line. Record any damage found during in-plant handling and correct the cause before finished goods accumulate.
At pre-shipment inspection, open sampled retail and master cartons. Compare actual materials, dimensions, marks, accessory restraint and product condition with the tested package. If a different carton or pallet pattern is used, document the change and assess whether the prior evidence remains relevant. Photograph the sealed and opened state, then re-pack sampled units correctly. The ToolViron quality overview can help connect the packaging check to the full shipment review.
Monitor destination damage after launch. A pattern of crushed corners, loose chargers or cracked cases can identify a weak point not reproduced in the initial test. Record carrier route, carton revision and lot. Then investigate the packaging and handling conditions, not just the damaged unit. A disciplined feedback loop can improve both protection and freight efficiency.
Caption: Illustrative shipment photography: every order needs its own approved inspection record.
A launch-packaging scenario
Suppose a private-label cordless drill kit includes a drill, two batteries, charger, bit set and molded case inside a retail carton. A prototype uses thick hand-cut foam, but the production proposal changes to a thinner molded insert to reduce cost. The buyer should not rely on the prototype's drop result. The parts have different masses and contact points; a loose charger or battery could strike the tool even if the outer carton remains intact. The production-intent insert should be assembled with real contents and evaluated under the chosen method.
Record the pre-test condition of every component. Are the batteries retained? Does the chuck touch the case wall? Are sharp bits held in a closed compartment? Is the manual separated from oily or abrasive parts? After the handling sequence, inspect each item and its location. A cosmetic scuff on the retail carton may or may not be acceptable by contract; a cracked charger housing or damaged battery is a very different outcome requiring qualified review and probably a package redesign.
Now imagine the kit is sold through both palletized distribution and direct-to-consumer parcel delivery. A master-carton test for pallet movement may not answer the parcel question. The buyer can request a separate assessment at retail-unit level, using a method suitable for that channel. It should not describe a pass at one level as proof for every route. This distinction should appear in the test report and packaging specification so future teams do not overinterpret the evidence.
If the new insert fails, change one element at a time where practical. A stronger divider around the charger may solve internal impact without increasing the entire carton size. A bar cover or blade shield may be more important for a chainsaw or planer kit. Retest the revised package and record its effective production lot. A cost-saving substitution should not be silently adopted after approval because it can make the original test irrelevant.
Questions to ask before accepting a packaging report
Which exact SKU and complete contents were tested? Was the pack assembled from production-intent materials? Which packaged level, method, sequence and sample count were used? What were the pre- and post-test acceptance criteria? Were functional checks performed by qualified personnel where needed? Were failures and retests retained in the file? A report that says only “drop test passed” cannot answer these questions and has limited value for a purchasing decision.
Ask whether the reported configuration includes the regional manual, plug, charger and export marks planned for the actual shipment. A later change to battery count or carton dimensions may warrant new assessment. Keep photos of the open pack and a bill of materials for insert pieces, not only an exterior view. If a retailer later reports damaged cases, the team needs to know what was tested and what was actually packed.
At shipment inspection, verify packing execution, not just design. Staff may place a charger in the wrong cavity or leave a cable pressed against a sharp edge. Sample cartons from different production periods and compare the arrangement with approved photographs. This is a simple operational check that protects the value of the more formal packaging test.
A packaging-cost boundary
Adding more foam or a thicker carton may seem like the safest response to a failed test, but it can raise freight volume, material cost and waste without protecting the specific vulnerable part. Use the damage evidence to identify where energy reaches the product, then change the relevant insert or orientation and retest. Document the new dimensions because the transport quote may change. A package is successful when it protects the approved kit through the chosen distribution channel at an acceptable total cost, not when it looks unusually heavy.
Frequently asked questions
Does one passed drop test guarantee no transit damage?
No. It provides evidence under stated conditions. Real distribution can involve different impacts, vibration, stacking and climate exposure. Choose a relevant method and continue monitoring arrivals.
Should the retail carton or master carton be tested?
That depends on the channel. A shipment may need evaluation at multiple packaged levels, especially when retail units later travel individually by parcel. Define which level each test covers.
Can a heavier kit use the lighter kit's test report?
Not automatically. Added batteries or accessories can change mass and internal movement. Assess and, where appropriate, retest the production-intent configuration.
What should a shipment inspector check after a package redesign?
Verify carton material and dimensions, inserts, product orientation, seals, labels, accessory restraint and finished-tool condition against the approved revision and test sample.
Conclusion
A useful carton test begins with the real saleable kit and the distribution route. Select a suitable protocol, inspect the product and carton after the complete sequence, correct identified weaknesses and control the tested design in production. Packaging is part of product quality, not a cosmetic last step.
Send your requirements
Share the tool category, kit contents, sales channel and planned transport route. ToolViron can discuss a packaging specification and pre-shipment review. Send your requirements to begin.
Images illustrate product and inspection topics; they are not documentary evidence of a specific ToolViron test or customer project. Confirm the exact model and market requirements before ordering.