A buyer sees a drill bit apparently orbiting rather than rotating on its own axis. Is the chuck defective? Possibly—but a bent bit, poorly seated shank, contaminated jaws or unstable test setup can produce a similar visual effect. A sample approval decision should separate those causes before it accepts or rejects a drill. It should also ask whether the observed movement matters for the actual hole-making task. A visible wobble on an extremely long bit is not the same observation as an out-of-position hole in a secured workpiece.
This guide describes a practical procurement check, not a universal runout tolerance. Agree any acceptance value with the supplier for the specific drill, chuck, test pin and measuring position. Keep electrical power isolated during fixture and manual-rotation checks, and let trained staff operate the tool only within its instructions. Starrett's indicator guide explains why a supported indicator can be used to assess runout, flatness or distance; the quality of the measurement still depends on the setup.
What does drill-chuck runout mean?
Runout describes the variation observed as a rotating surface turns relative to a reference axis. For a drill sample, a buyer may inspect the chuck exterior, a straight test pin held in the jaws or a fitted drill bit. These are different measurements. Total indicator reading is the difference between the highest and lowest readings at the chosen contact point during a controlled rotation. It should not be reported as an undefined “accuracy percentage.”
The farther the indicator is from the chuck, the more a small angular error or bent accessory can affect the reading. That is why “measured at the tip” without naming the pin length is not a comparable specification. A factory test record should state the test pin size and condition, insertion depth, distance from chuck face to indicator, fixture arrangement, measuring instrument and repeated results.
Hole accuracy is broader than spindle or chuck runout. Material movement, point geometry, bit wear, pressure, speed, pilot marking and a user's hand position can all move the finished hole. A useful buyer review therefore includes both a controlled bench measurement and a workpiece test reflecting the target customer's task. Neither alone proves everything.
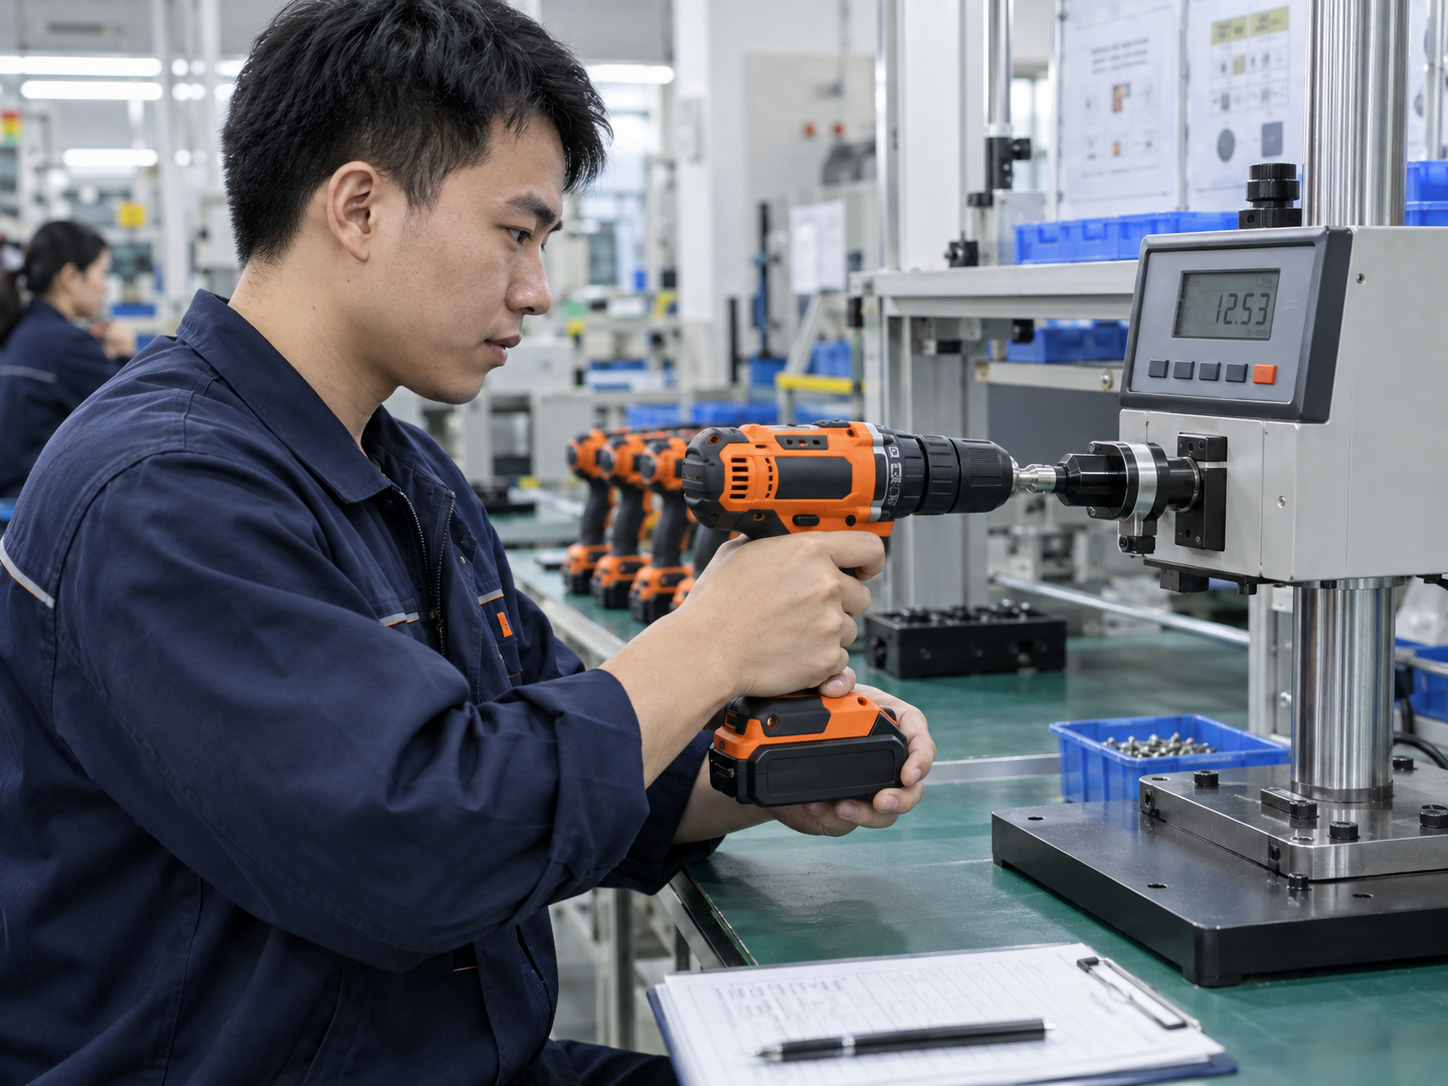
Caption: A runout number is only useful when the accessory and measuring position are defined.
Prepare a repeatable sample
Begin with a representative drill and the exact chuck variant intended for sale. Check its model, revision, jaw opening and approved accessory interface against the purchase specification. Look for shipping damage, a loose sleeve or obvious jaw irregularity. If the sample is damaged, document that condition before treating it as a design characteristic. Use more than one sample when deciding whether a pattern exists.
Select a clean, straight, verified test pin whose shank is appropriate for the chuck. A production drill bit is helpful for a real-use test but is a poor sole reference for geometric measurement: flute shape, point grind and prior damage can add variation. Seat the pin to the defined depth and tighten the chuck according to its instructions. Avoid gripping a polished or tapered area that the jaws were not designed to hold.
Secure the drill body in a purpose-made fixture without distorting its housing or switch. Mount the indicator to a stable base independent of the tool. Bring the contact to the agreed position and rotate the chuck manually only if the tool design and safety procedure permit it. Do not power a drill against an indicator probe or reach around a moving chuck. Record the high and low readings, then remove and reseat the pin and repeat. If results change markedly, seating or chuck-jaw condition may be contributing.
Consider a second pin diameter within the chuck's intended range. Some faults appear only when the jaws close near one end of their travel. Do not assume a chuck is sound because one convenient pin size produced a small reading. Equally, do not demand an unrealistic metrology value that the end user's drilling application never needs. The test must be tied to the product position.
Separate the possible sources of movement
If the pin runs out, first clean and reseat it. Then check the pin itself against a reliable reference and inspect the jaws for debris or uneven contact. A bent pin or a shank gripped at an angle can produce a dramatic reading on a good chuck. If the reading follows the pin orientation when the pin is rotated in the jaws, suspect the pin. If it follows the same chuck-jaw position through different verified pins, investigate the chuck.
The chuck mounting and spindle may also matter. Do not disassemble a new tool in a routine purchasing review; that can create hazards and invalidate the sample. Instead, record the symptom and ask the manufacturer to investigate with its own controlled method. A buyer can request a cause explanation, corrective action and a new production-intent sample. It should not write “spindle bent” into a report merely because a bit appears to wobble.
The drill bit is another variable. A long, narrow bit can deflect under side pressure. A masonry bit may not have a point geometry intended for the same positional accuracy as a suitable metal-drilling bit. Use the accessory suited to the application and compare like with like. The existing drill-bit material matching guide helps define this part of the brief.
Test the result in a real workpiece
After the geometry check, choose a task the customer actually performs. For furniture assembly, that might be a marked pilot hole in a consistent board. For light metal fabrication, it might be a clamped steel coupon with a specified center mark and bit. Define material grade and thickness, bit type and condition, drill speed setting, clamping, operator and number of holes. These details matter more than a photograph of one successful hole.
Measure hole position and quality with a suitable gauge or template. Look for oversize entry, wandering, burrs or irregular finish as relevant to the task. Repeat with several sample drills and new, matched bits. A single skilled operator can compensate for a weak tool; use a consistent procedure and, where the channel serves casual users, consider a first-use assessment after the controlled test. Do not turn operator skill into a falsely precise factory claim.
Compare the same tool with different appropriate bits if the result is unexpected. If holes improve dramatically with a verified accessory, the accessory bundle may be the commercial issue. If all appropriate bits show the same defect, request a manufacturer investigation. The buying decision should distinguish tool body, chuck, supplied bit and intended task.
Write an acceptance rule that can be inspected later
An acceptance rule should name the test method, not simply “chuck must be accurate.” It might identify a test pin of stated diameter and length, clamping depth, measuring position, maximum total indicator reading, number of units and retest rule. Then add a functional hole-quality check on the intended material. The numerical limit must come from product engineering, customer requirements and agreed manufacturing capability; this article does not supply one.
Include who maintains the pins and indicators. A worn reference pin or an indicator knocked out of calibration can make a good production lot look poor or hide a real problem. A factory test sheet should record instrument ID, sample serial or lot, operator, date and disposition. If a result exceeds the limit, keep the original observation and the investigation, not only the retest number.
For shipment inspection, ask whether the final inspector can perform the same controlled check or whether a simpler functional screen is more appropriate. A third-party inspector with no fixture should not invent a hand-held “wobble test” and call it the agreed TIR method. The shipment plan can instead verify chuck operation and sample appearance while reviewing the factory's recorded metrology results.
Mid-article sourcing CTA: Seeing inconsistent hole quality in drill samples? Send the chuck type, bit size, workpiece and current measurement method for a specification and sample-review discussion.
Use complaints as measurement clues
After-sales reports often use “wobble” to describe different problems. Ask whether it occurs with one bit or all bits, at the tip or near the chuck, with no load or only in material, and whether the chuck grips the shank securely. Request a short video only if it can be captured safely with the tool stationary or operated according to instructions. Never ask a customer to hold an indicator against a running bit.
Record accessory make and condition, installation method and drill model. If a customer reports a wandering hole, check the workholding and material as well as the tool. If a chuck releases a bit or jaws fail to close evenly, treat that as a separate issue. Distinct fault codes help the supplier investigate genuine quality patterns rather than responding to a mixed pile of returns labelled “chuck bad.”
A documented lot comparison can reveal whether the issue began after a component or assembly change. That connects this test to supplier change control and prevents an approved sample from becoming a false reassurance after production differs. Keep the product configuration and test method aligned as both evolve.
Interpret a measurement before rejecting a lot
Consider a batch where one sample gives a larger TIR reading than the other units. The first response should be to verify the instrument setup, pin and seating, then repeat the measurement on that same unit. If the result remains high, mark the unit and check additional samples from the same production period. A single outlier can indicate an individual assembly problem; a cluster can indicate a tooling, chuck-supplier or process shift.
The buyer should agree how many units trigger containment and who decides disposition. A vague instruction to “check more pieces” can delay shipment without resolving risk. Define whether the concern is a safety-related retention failure, a hole-quality issue or a cosmetic observation. Each has a different severity and evidence threshold. The factory should keep original readings, not replace them with a later adjusted value.
An important distinction is repeatability versus reproducibility. Repeatability asks whether the same operator and fixture give similar readings on the same unit. Reproducibility asks whether another trained person or station can obtain a comparable result. If neither is established, a tight tolerance may be impossible to enforce fairly. The buyer can require a simple measurement-system study before attaching financial penalties to a number.
Explain the result to customers without jargon
Most customers do not need to hear about indicator preload or spindle datum. They need to know whether the drill holds a suitable bit securely and can make holes of the quality claimed for the task. A product page should describe chuck capacity and intended application; it should not claim “zero wobble.” No rotating assembly is described usefully by an absolute visual promise.
For high-precision applications, state the real limitation and suggest a more appropriate machine when a handheld drill cannot meet it. If the tool is aimed at installation rather than machining, a carefully bounded hole-placement trial is more honest than a laboratory-style claim with no field relevance. Good technical communication protects the buyer's reputation by telling customers where the product fits.
A final evidence boundary
The inspection result should not be marketed as a general precision guarantee. It applies to the defined sample, accessory, fixture and task. If the buyer later bundles a longer bit or changes the chuck supplier, review the original evidence before repeating the claim. A concise statement of limitations is not weakness; it tells a trade customer what was actually checked.
Frequently asked questions
Is visible drill-bit wobble always a defective chuck?
No. A bent or long bit, poor seating, debris in the jaws or a loose test fixture can also create visible movement. Check a verified straight pin and repeat the seating before assigning a cause.
What is total indicator reading on a drill?
It is the range between the highest and lowest indicator values during one controlled rotation at a stated measuring position. Without the pin and setup details, two TIR numbers may not be comparable.
Can a drill have low runout but still make inaccurate holes?
Yes. Bit geometry, material, clamping, marking, feed force and operator technique affect hole position and finish. A functional workpiece test complements a bench measurement.
Should every finished drill be tested with a dial indicator?
That depends on product design, risk and the agreed control plan. A factory may use process controls and defined sampling while checking each unit for basic chuck function. Buyers should agree the evidence needed for the intended channel rather than assume one universal inspection frequency.
Conclusion
A useful drill-chuck review separates geometric measurement from finished-hole performance. Control the pin, seating and fixture; investigate variation; and connect acceptance criteria to the real job. This prevents a buyer from rejecting good product because of a poor accessory—or accepting a weak chuck because one demonstration hole happened to look straight.
Send your requirements
Share the drill model, chuck variant, intended bit range and the hole-quality issue you need to resolve. ToolViron can discuss a repeatable sample check and the factory evidence required before shipment. Send your requirements to start.
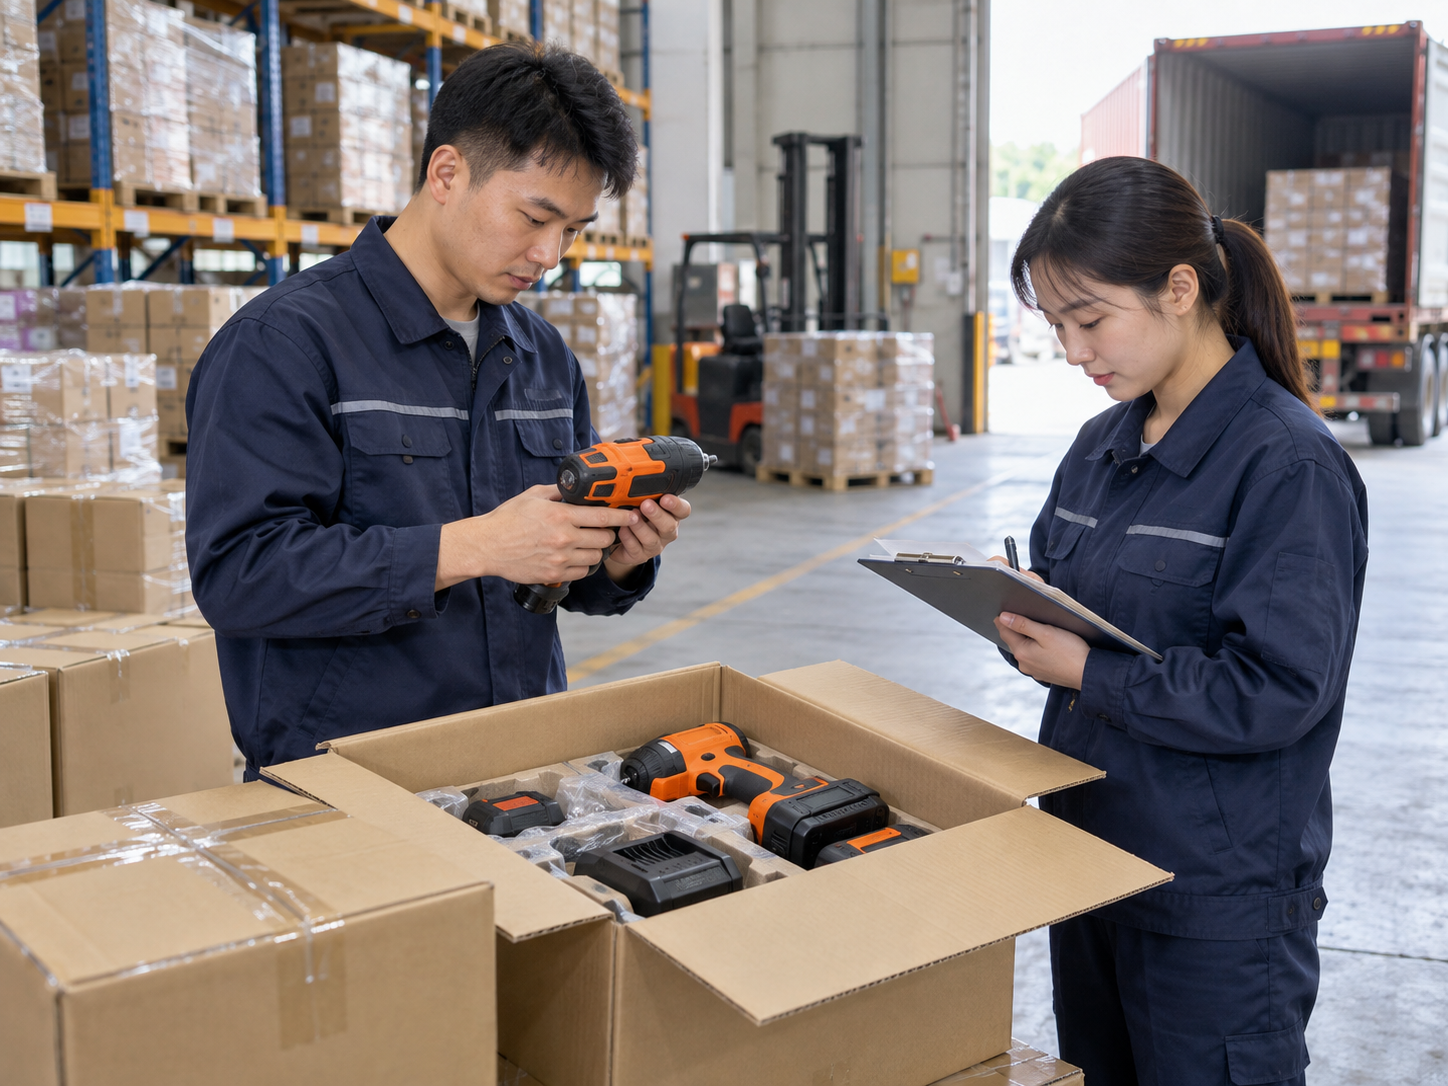
Caption: Documented sample and shipment checks help preserve the approved chuck configuration.
Images illustrate product and inspection topics; they are not documentary evidence of a specific ToolViron test or customer project. Confirm the exact model and market requirements before ordering.