An approved hand-built sample is an important milestone, but it is not the same as a repeatable production route. A private-label drill may look right on a product table while the line discovers that the regional plug does not fit the insert, the accessory bag is easy to omit or the final test fixture cannot accommodate the chosen case. A small production-intent pilot run is the bridge between sample approval and volume manufacture.
The term “first article inspection” is used in quality practice for inspecting the first item or group produced from a run; ASQ's supplier-quality handbook sample provides that context. A buyer should not assume a particular industry form is required for every power tool. Define a pilot gate proportionate to the tool, market and order risk.
Define what the pilot is meant to prove
A pilot should answer whether approved parts, instructions, process steps, tests and packing can be reproduced using the intended line and operators. It is not merely another marketing sample. Agree the pilot quantity, manufacturing location, line setup, component lots, software or electronics revision where relevant, and what will be inspected. The goal is to find process problems while the correction is still manageable.
Separate design approval from process approval. A product may be technically acceptable but difficult to assemble without damaging a cable, misplacing a spring or confusing two similar accessories. Conversely, a smooth assembly line can repeatedly produce the wrong market label if the specification was never clear. The pilot must test both the product and the route.
The earlier sample approval guide explains how to select a reference product. This article begins after that decision and asks whether a small batch produced under intended conditions matches the reference.
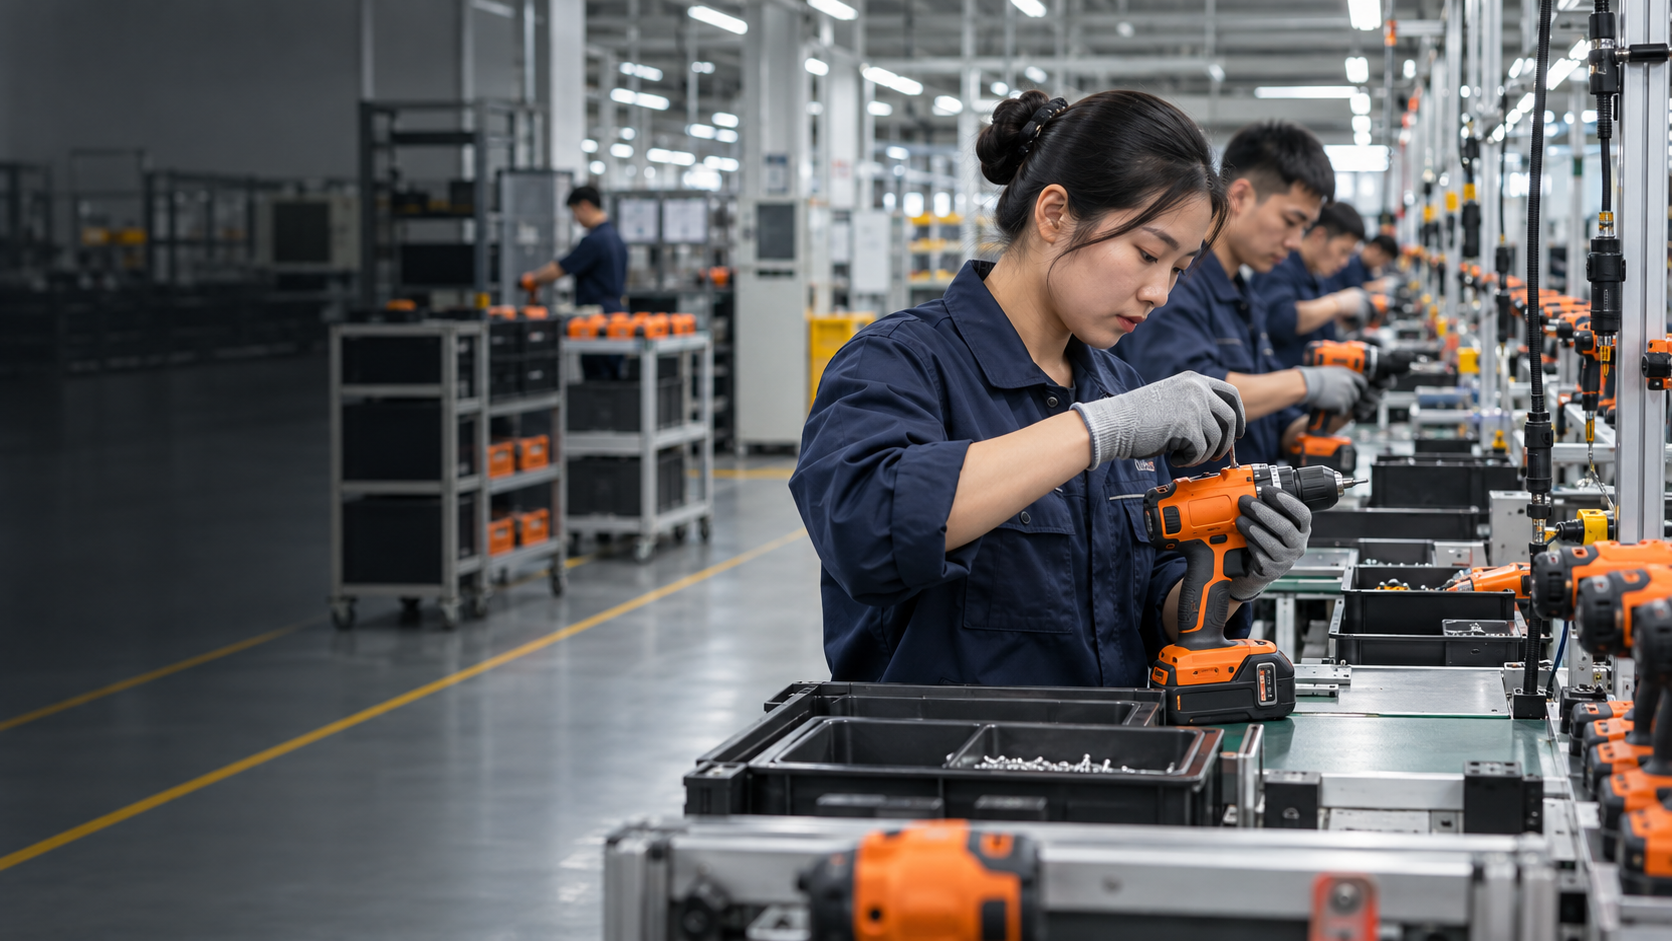
Caption: A pilot batch tests the repeatability of the production route, not only one showroom sample.
Freeze the input package
Before scheduling the run, release a controlled bill of materials, drawings or specification, approved sample, test criteria, artwork, manuals and packing instruction. Identify any open deviations. A pilot that uses temporary parts or handwritten labels may be useful engineering work, but it should not be called production-intent without a clear gap list.
Record component supplier and lot for safety-related and customer-visible parts. On a drill that may include chuck, switch, cable or battery; on a grinder, guard and flange; on a chainsaw, bar and chain; on a planer, blade and sole. The exact list depends on the product. If a supplier changes a part during the pilot, pause and record the deviation rather than hiding it inside the finished sample.
The regional configuration must be complete. Check plug or charger, voltage identification, language, supplied accessories, carton marks and importer's requested information. A good pilot for one market is not automatic evidence for another SKU with a different power or documentation package.
Observe the line as work happens
Walk through material picking, subassembly, final assembly, functional testing, visual inspection and packing. Record where operators need to guess or rework. Are two screws nearly identical? Can a cable be routed two ways? Does the fixture reject a good tool because it expects the old accessory? Process ambiguity is the pilot's most valuable finding.
Use a defined inspection sheet that can link results to each unit or sampling group. Include the critical dimensions or functional checks agreed for the model. Inspect a few units from the beginning, middle and end of the run rather than selecting only the best-looking first piece. A defect that appears after a fixture warms up or material replenishment may not show at the start.
Do not reward a flawless pilot report if hidden rework was needed. Log defects, corrections, cycle interruptions and scrap honestly. The purpose is to make volume production dependable, not to create a document that says “all passed” while engineers quietly rescued every unit.
Test the finished kit, not just the tool body
Open pilot cartons and compare contents with the approved bill of materials. Inspect manual revision, label, accessory count, plug or charger, case insert and carton orientation. Conduct any agreed functional or application checks on units selected after packing. A tool may pass the line's electrical test yet ship with the wrong side handle or replacement chain.
The manual and label localization guide helps buyers review destination-market information. The pilot is a good moment to see whether the printed result is readable and positioned correctly on the physical product, not just approved as a PDF proof.
If a drop or transport assessment was planned, use the final pilot kit and packaging, including batteries and accessories. A test on an earlier empty case or a lighter variant does not automatically cover the saleable shipment. The carton drop-test article explains that boundary.
Set a release gate before the run starts
Define who can approve the pilot and what evidence they need. Possible inputs include measured results, defect log, revised work instructions, sample cartons, artwork approval and unresolved-issue list. Severity matters: a missing decorative insert may be corrected differently from a guard fit problem or wrong electrical rating. The acceptance rule should not be invented after the factory has produced a batch.
If an issue is found, assign owner, containment, cause review, correction and verification. Some corrections can be checked on a small set; others require a new pilot or renewed lab assessment. The buyer and supplier should agree which deviations are permitted in a controlled early shipment, if any, and which block mass production.
Keep the approved pilot units and records as production references. They should be identifiable by model, revision and date, with clear storage conditions. A “golden sample” that is later modified or stripped for parts loses its value. The lot-traceability guide explains how production identity carries forward.
Mid-article sourcing CTA: Moving a private-label tool from sample to production? Send the approved configuration, target market and first-order size for a pilot-gate discussion.
Translate findings into repeat production controls
A pilot result is useful only if lessons change the line. Update pick lists, fixture settings, operator instructions, training and inspection points. If the manual pack was repeatedly missed, change the physical packing process rather than only reminding operators. If a test fixture created false failures, calibrate or redesign it and retain the original incident record.
Agree a start-of-run verification for later repeat orders. A successful pilot from six months ago does not prove a new component lot or a new shift will behave identically. The factory can inspect first pieces, confirm material revisions and review test equipment before full output. Buyers should include this expectation in repeat-order planning.
Do not make the pilot a blanket guarantee of every unit's future quality. It is evidence of readiness at a point in time under defined conditions. Incoming inspection, in-process control, final testing and shipment inspection remain necessary according to the agreed plan.
Communicate the outcome to commercial teams
Sales and procurement teams need a concise release note: approved model, variants, pilot date, tested configuration, remaining caveats and next action. Avoid circulating raw engineering notes without a clear decision. If a market variant was not piloted, say so explicitly. This prevents a buyer from assuming that a different plug or accessory bundle was already validated.
Use the pilot to refine the quotation. A discovered packing insert, test step or accessory change may affect cost and lead time. It is better to surface that before mass production than absorb a hidden substitution later. The landed-cost comparison guide supports a whole-programme view.
Keep customer-facing claims tied to real evidence. The pilot may demonstrate that a particular assembly route can be repeated; it does not prove a universal lifetime or every application. Do not call an illustrative factory photograph a documentary record of this specific run.
Use a pilot issue log that forces decisions
For each finding, record unit or carton identity, station, observed condition, expected condition, severity, temporary containment, owner and verification result. A photograph helps only when it is linked to a part or station. “Packing wrong” is too vague; “two of 30 sampled cartons contained the previous manual revision after a changeover” can be investigated and corrected.
Separate open issues from accepted deviations. A buyer may allow a cosmetic carton mark in pilot units while blocking a wrong plug or guard. The decision should be signed by the responsible product and quality owners and should specify whether the affected pilot units can be sold. Do not allow a verbal “we will fix it next time” to convert a safety or market-identity issue into a released order.
After correction, run a focused confirmation on new units. Reworked original units may show that the correction can be performed, but newly assembled units show whether the process itself has improved.
Check changeovers, not just steady production
Many mistakes happen when a line switches from one regional variant to another. A pilot that produces only one long run may miss wrong manuals, plugs or carton labels after changeover. If the first order includes several markets, plan a small controlled transition and verify the first pieces of the next variant. Record clearance of old materials from the station.
The same applies to material replenishment during a run. A new carton of switches or handles can contain a different lot or part. Compare the incoming identifier with the approved pick list and observe whether line staff can detect a mismatch. This is an operational control, not a theoretical supplier audit.
The buyer can use the pilot to decide whether variant complexity exceeds the line's current controls. It may be better to separate packing runs or add scanning than to rely on workers recognizing nearly identical parts by eye.
Link pilot evidence to the customer requirement
Each critical customer requirement should have a visible confirmation route. If the customer asked for a specific chuck, guard, chain or planer blade, identify where the pilot checks it. If the customer asked for market-language documentation, inspect the physical leaflet and product label. If a performance claim is planned, reference the relevant product-specific test rather than a generic functional spin.
This mapping prevents a common gap: the factory produces a rich inspection folder, yet none of its measurements answer the buyer's actual concern. A concise requirement-to-evidence table can be reviewed before the run. Any requirement that lacks a check should be assigned an owner or explicitly marked as outside the pilot scope.
The evidence should be retained in a format that can be reused on the next order. A photograph with no SKU or date is hard to compare six months later; a controlled report with configuration and method remains useful.
Make the next-order rule explicit
After a successful pilot, define what must be rechecked for repeat orders. New component suppliers, tooling maintenance, revised artwork, another market or a long production gap can change the risk. A repeat order need not rerun every pilot step, but it should confirm inputs and first pieces before volume output.
Write a short release summary with approved part revisions, known process settings, inspection frequency and escalation contacts. Purchasing should attach this to the order rather than rely on a memory of the original project. If the supplier proposes a substitution, the buyer can compare it against the controlled pilot record and decide whether renewed testing is needed.
One final release condition
The pilot is complete only when its open issues have an agreed disposition and the line instructions reflect the accepted corrections. A signature on a sample photograph is not a process release. The buyer should be able to point to the approved configuration, pilot record, remaining caveats and start-of-run check for the next order.
Frequently asked questions
Is a hand-built approved sample enough to start a large OEM order?
It may be enough for a simple programme only after the parties assess risk, but a production-intent pilot can reveal line, testing and packing issues that a hand-built sample cannot. Define the gate proportionately.
How many units belong in a pilot run?
There is no universal count. Choose enough to exercise the intended line, material replenishment, inspection and packing steps for the product risk. Record the basis for the chosen quantity.
Can temporary components be used in the pilot?
They can support engineering learning, but the run should be labelled accordingly. List gaps and verify the final production parts before calling the configuration approved.
What should block mass-production release?
Unresolved safety-related, functional, compliance, critical fit or market-identity issues should be reviewed by responsible specialists. The buyer and supplier should define severity and disposition before the pilot begins.
Conclusion
A pilot run turns an approved product idea into a repeatable manufacturing question. Freeze inputs, observe real assembly and packing, record defects honestly and use a pre-agreed release gate. The result is not a ceremonial certificate; it is a practical decision about whether the OEM programme is ready to scale.
Send your requirements
Share the product category, approved sample status and target order. ToolViron can discuss a pilot-batch and inspection plan aligned with your market configuration. Send your requirements to begin.
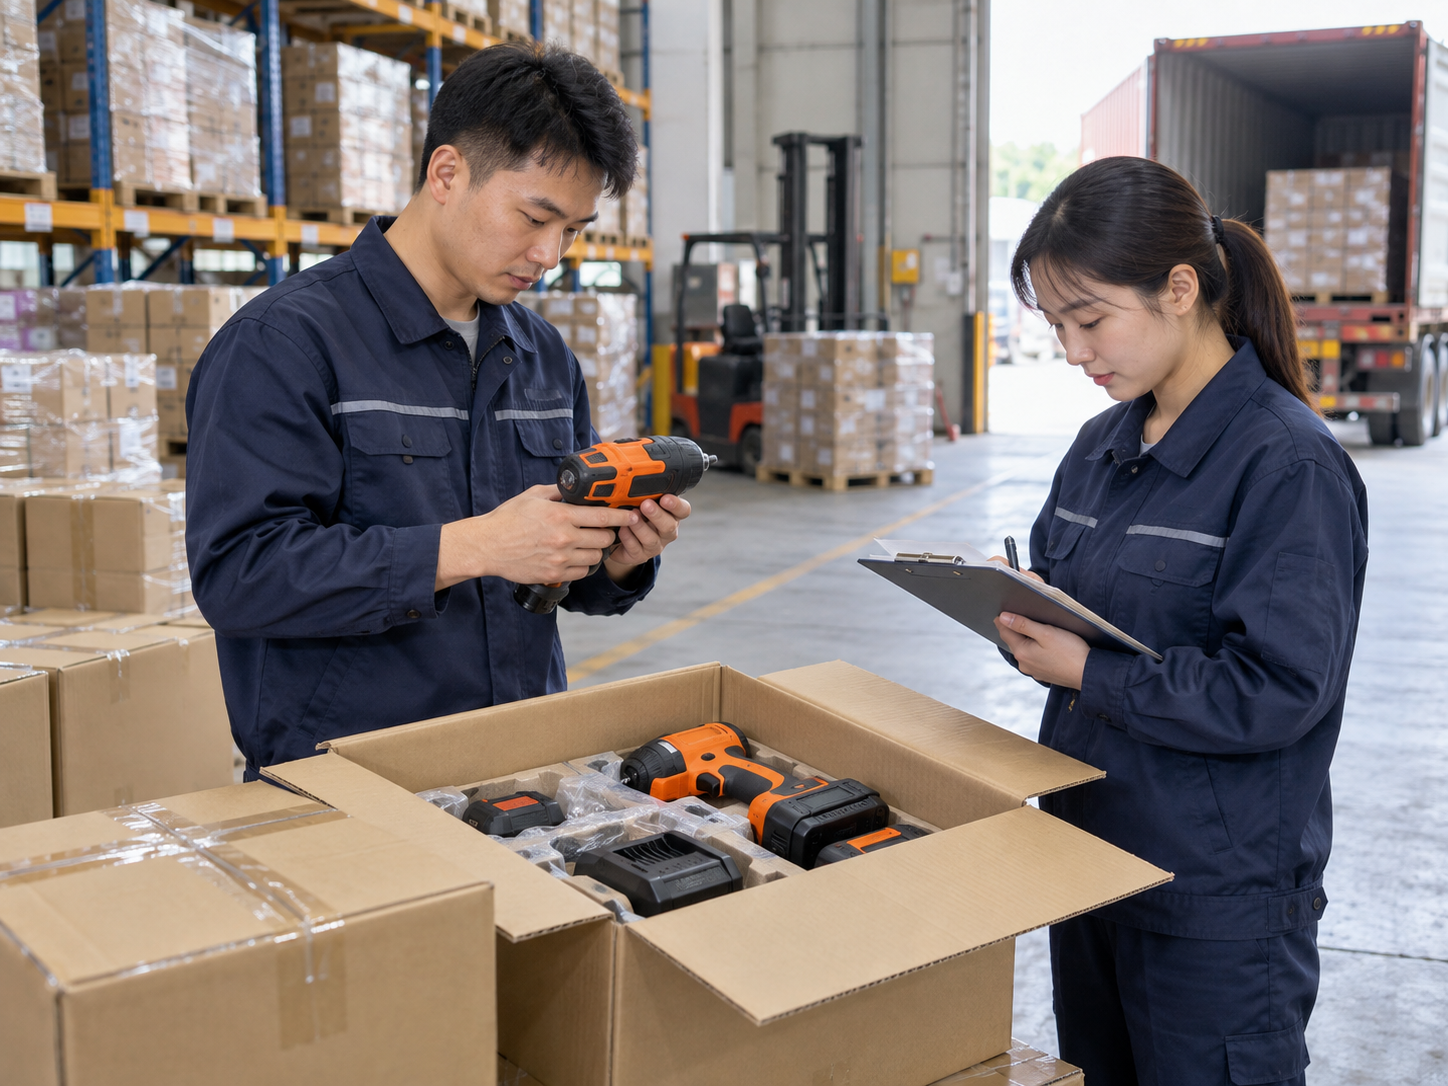
Caption: The pilot decision should include the packed product customers will actually receive.
Images illustrate product and inspection topics; they are not documentary evidence of a specific ToolViron test or customer project. Confirm the exact model and market requirements before ordering.